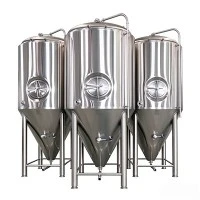
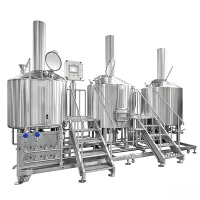
The CO₂ Recovery System for Beer Production is a gas recovery system specifically designed for beer production. It is used to recover carbon dioxide from the fermentation process, purify, liquefy, and store it for reuse in beer carbonation, oxygen displacement during canning, and other brewing processes.

System Components
CO₂ Collection System
Fermentation Tanks – Captures CO₂ directly from fermenters using gas-tight collection systems.
Pressure Control Valves – Maintain optimal pressure (typically 0.2–0.5 bar) to prevent oxygen ingress.
Gas-Liquid Separators – Remove moisture and foam before CO₂ enters the recovery system.
Pre-Treatment & Filtration
Activated Carbon Filters – Remove organic impurities such as ethanol, esters, and sulfur compounds.
Particulate Filters – Eliminate yeast and hop residues.
Deodorization Unit – Ensures CO₂ is odor-free and suitable for reuse in beer production.
Compression & Cooling
Multi-Stage Compressors – Increase CO₂ pressure up to 20–30 bar for liquefaction.
Intercoolers & Aftercoolers – Reduce gas temperature after compression.
Drying System – Adsorption dryers (e.g., silica gel or molecular sieves) remove residual moisture.
Liquefaction & Storage
Refrigeration Unit – Cools CO₂ to -25°C to -30°C for liquefaction.
Condenser – Converts gaseous CO₂ into liquid form.
Liquid CO₂ Storage Tank – Insulated, pressurized vessel (typically 15–20 bar) for holding purified CO₂.
Reclaiming & Distribution
Evaporator – Converts liquid CO₂ back to gas for brewery use.
Piping Network – Distributes CO₂ to:
- Carbonation Tanks
- Bottling/Canning Lines
- Tank Purging Systems
Monitoring & Safety Systems
Gas Analyzers – Continuously monitor CO₂ purity (≥99.9%, food-grade standard).
Pressure Relief Valves – Prevent over-pressurization.
Emergency Venting – Safely releases excess CO₂ when necessary.
Parameter
1. Production Capacity Parameters
| Parameter | Small Brewery | Medium Brewery | Large Brewery |
|---|---|---|---|
| Annual Output | 1,000–10,000 HL | 10,000–500,000 HL | 500,000+ HL |
| Batch Size | 10–50 HL | 50–500 HL | 500–2,000 HL |
| Fermentation Time | 5–14 days | 5–10 days | 4–8 days |
2. CO₂ Recovery System Parameters
| Parameter | Specifications |
|---|---|
| CO₂ Yield (per HL beer) | 2–3 kg/HL (from fermentation) |
| Recovery Efficiency | 70–90% (of total CO₂ produced) |
| Purity Standard | ≥99.9% (food-grade, EIGA/ISBT) |
| Storage Capacity | 1,000–50,000 kg (liquid CO₂) |
| Compression Pressure | 20–30 bar (for liquefaction) |
| Liquefaction Temp. | -25°C to -30°C |
Feature
High-Purity CO₂ Recovery
Through multi-stage filtration, activated carbon adsorption, and deodorization treatment, the system can purify the CO₂ produced during fermentation to food-grade standards (≥99.9%).
Reduced Operating Costs
Recovering CO₂ from fermentation reduces reliance on purchased CO₂, saving procurement costs.
Automated Control
PLC automated control and real-time monitoring systems simplify operation procedures, reducing human error and maintenance costs.
Safe and Reliable
Equipped with pressure relief valves, emergency discharge systems, and gas analyzers, the system continuously monitors CO₂ purity and pressure, ensuring safe and reliable operation.
Packing and Delivering

Certificate
As a professional CO2 Recovery System For Beer Production manufacturer, our products have passed CE and PED certifications, pressure vessel equipment certification, and obtained more than 30 patent certifications.

Customer Review

Hot Tags: co2 recovery system for beer production, China co2 recovery system for beer production manufacturers, suppliers, factory